Private label rubber pet toys are a common category for retailers and distributors that want brand control, unique designs and margin flexibility. For B2B buyers, sourcing these products means more than picking a shape and logo: decisions on material declarations, molding interfaces, tooling type, color controls, sample verification, packaging and QC strategy determine cost, lead time and regulatory fit for target markets. This guide focuses on practical buyer actions, the supplier inputs you should request, the evidence to accept, and the tradeoffs you will face.
This article is Part 1 of a modular sourcing checklist intended for buyers who will manage specification, supplier evaluation and product launch planning. It avoids unverified technical claims about rubber performance and does not substitute for market-specific legal or safety advice. Buyers should confirm target-market requirements and labeling or testing mandates with their own compliance experts 3.
Module 1 — Define product role and customer expectations: decide primary function, use-case and retail positioning
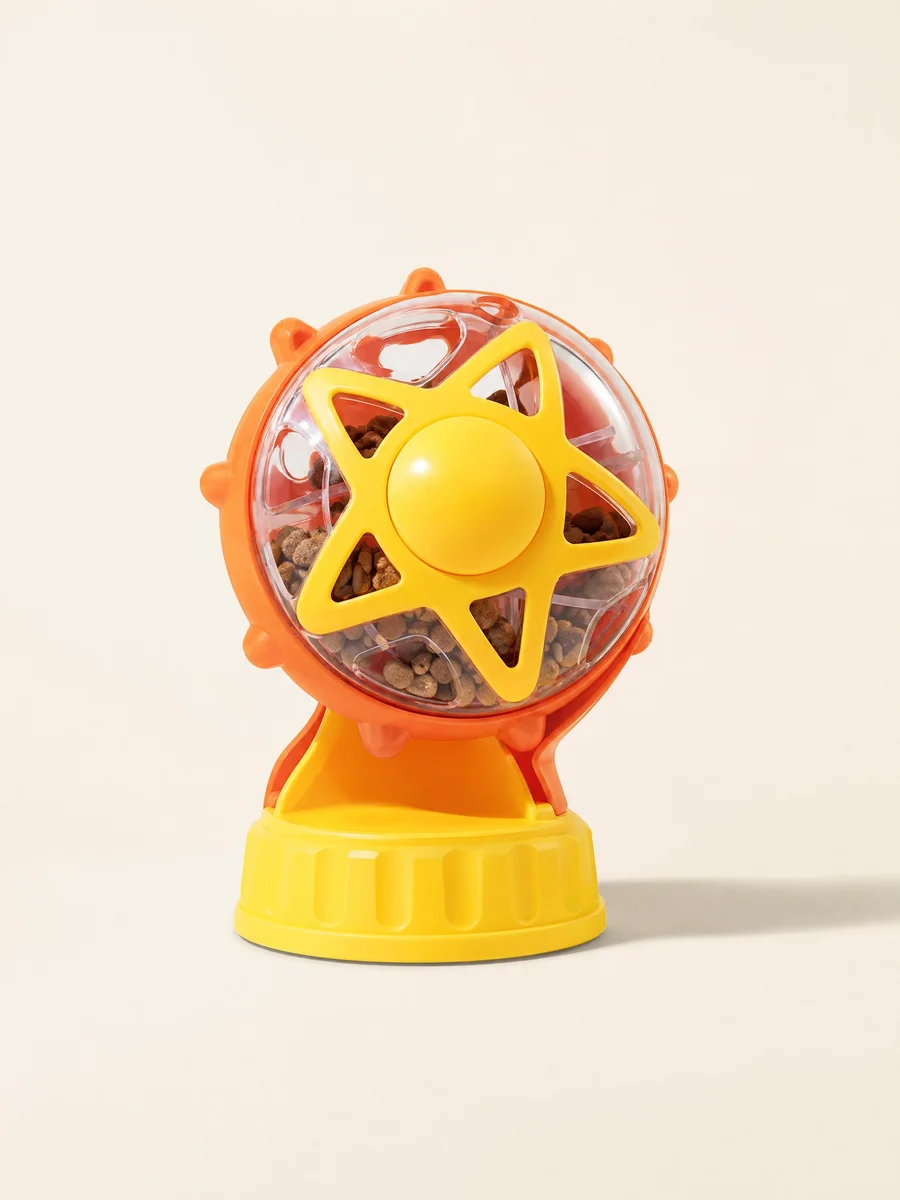
First, clarify the toy’s primary role (chew, fetch, treat-dispensing, dental-texture, or multi-function). This decision drives choices in geometry, wall thickness, molding complexity and acceptable materials. Action for the buyer: prepare a brief that states intended age/size of animal, typical use scenarios (indoor/outdoor, supervised/unsupervised), expected retail price band and any competitive references. Supplier input to request: recommended geometries for the stated function, past factory experience with similar SKUs, and any production limitations (e.g., minimum-feature size, maximum undercut depth).
Evidence to accept from suppliers includes CAD or 3D render previews annotated with critical dimensions and suggested tolerances, and a written acknowledgement of use-case assumptions. Tradeoffs: simpler single-cavity molds reduce unit cost and speed up sampling but limit surface/feature options; complex family molds save per-piece cost at high volume but increase initial tooling risk. Next steps: finalize the use-case brief and obtain comparative supplier proposals with identical scope so you can evaluate tooling and per-unit cost consistently.
For quick comparison, use this compact table to record primary function parameters across candidate SKUs:
| SKU / Concept | Primary function | Target dog size/age | Retail price band |
|---|---|---|---|
| Concept A | Chew / heavy | Large adult | Mid |
| Concept B | Treat-dispensing | Small/medium | Premium |
| Concept C | Fetch / buoyant | All sizes | Value |
And capture supplier feasibility notes in a simple procurement table:
| Supplier | Suggested mold type | Minimum feature size | Production constraints |
|---|---|---|---|
| Supplier X | 2-cavity injection | 1.0 mm | Max undercut 3 mm |
| Supplier Y | Blow-mold + overmold | 0.8 mm | No steel inserts in soft area |
Module 2 — Geometry, molded interfaces and assembly decisions: settle critical geometry and how parts come together
Geometry and molded interfaces determine whether the toy can be produced in a single operation or requires multi-step molding, overmolding, inserts or post-assembly. Buyer actions: define critical functional dimensions (gap widths, internal chambers, mating faces), specify which surfaces must be free of flash, and declare whether the final SKU may include secondary parts (screws, metal rings, squeaker units). Supplier inputs to request: draft-angle recommendations, required mold shut-off surfaces, and proposals for gating/runners relevant to the chosen geometry.
Evidence for acceptability includes annotated 3D CAD files with tooling split planes, and a plan for how to integrate any secondary components (e.g., ultrasonic welding zones, adhesive areas or mechanical interlocks). Tradeoffs: designing for a single-cavity, single-shot process minimizes leak points and can improve durability but may constrain internal geometries; designing for assemblies allows functional complexity (like treat dispensers) but adds inspection steps and higher reject risk. Next steps: finalize a CAD master that includes tooling splits and hand it to shortlisted suppliers for DFM (design for manufacturing) reports.
Use this table to log supplier DFM feedback on geometry and interfaces:
| Feature | Requirement | Supplier A comment | Supplier B comment |
|---|---|---|---|
| Internal chamber diameter | 20 ± 0.5 mm | Needs bevel for demolding | OK with slide core |
| Squeaker pocket | Press-fit | Recommend adhesive | Use insert molding |
Module 3 — Material selection and declarations: choose materials and require supplier documentation
For private label rubber pet toys, buyers must choose materials that align with product role, visual goals and regulatory expectations for target markets. Buyer actions: specify acceptable material families (e.g., thermoplastic elastomer grades, natural rubber, silicone elastomers) and require suppliers to provide full material declarations and supplier chain details for each grade proposed. Supplier inputs to request: material technical datasheets from the compounder, material identification (trade name, grade), and origin or supplier name for the compound.
Evidence to accept: material datasheets plus a supplier-signed material declaration that links the compounder’s trade name to the finished material used in the SKU. Avoid accepting only marketing names without a clear compound and supplier. Tradeoffs: TPEs often simplify molding and color matching, while other elastomers can offer different tactile properties; however, buyers should avoid basing decisions on unsupported performance claims and instead define measurable acceptance criteria (e.g., shore hardness range, elongation requirement) that the supplier must document. Next steps: include material trade name, manufacturer contact and required physical parameters in your purchase specifications and require material traceability to be kept with production batches.
Record material proposals and declarations in a supplier material log:
| Supplier | Proposed material | Trade name / compounder | Key declared parameter |
|---|---|---|---|
| Supplier X | TPE | TPE-123 (Compounder Y) | Shore A 60–70 (declared) |
| Supplier Y | Silicone | SIL-Soft (Compounder Z) | Food-contact grade claimed |
Module 4 — Tooling questions and approvals: confirm mold ownership, revisions and sample policy
Tooling decisions affect cost allocation, lead time and long-term flexibility. Buyer actions: decide who will own the tooling (buyer-paid, supplier-paid, or cost-shared), define revision policy (how many free revisions are allowed, who bears revision costs) and request a tooling approval workflow with milestones. Supplier inputs to request: tooling lead time, a tooling P0/P1/P2 sample plan (explained below), and a clear quote for mold costs and lifecycle expectations.
Evidence to accept includes a written tooling agreement that specifies ownership, expected cavity life, warranty terms for first runs, and an approved first-article inspection (FAI) checklist tied to the master CAD. Tradeoffs: buyer-paid tooling gives the brand more control and the ability to move molds, but it increases upfront CAPEX; supplier-funded tooling can lower initial costs but may limit future negotiations or movement of tooling. Next steps: agree a tooling contract annex with change control and a sample approval matrix so both parties understand when production can begin.
For tooling/sample workflows, log key milestones:
| Milestone | Deliverable | Responsible party |
|---|---|---|
| Mold release | Tool inspection photos + cavity count | Supplier |
| P0 sample | First-shot samples for dimensional check | Supplier |
| P1 sample | Production-simulated runs for cosmetic check | Supplier |
| P2 sample | Pre-production batch for packaging and function check | Buyer/Supplier |
Mid-article CTA — If you want PawViso to coordinate supplier DFM and tooling milestones, request a tooling checklist and sample-plan template from our team. We can share a neutral sample-report format you can use with any supplier.
Module 5 — Color controls, sampling and acceptance criteria: set tolerances and a reproducible sample process
Color consistency is a common pain point for private label items. Buyer actions: define color targets using a measurable standard (Pantone or lab color targets) and a tolerance method (delta E threshold with lighting/observer conditions) that the supplier must meet. Request initial color chips and a molded color reference sample retained by the supplier and by you as the master reference. Supplier inputs to request: pigment and masterbatch source, color-match process steps, and whether pigments are pre-dispersed or mixed in-house.
Evidence to accept: a molded color reference sample that has been produced under steady-state process parameters and a signed color approval form that lists the accepted delta E threshold and measurement method (spectrophotometer model, light source). Tradeoffs: tighter delta E tolerances increase rework and cost, and natural pigments may change shade across lots; agree realistic tolerances linked to retail expectations. Next steps: include color-maintenance procedures in your production contract and require that suppliers retain a sample per lot for comparison.
Also specify sampling frequency and acceptance criteria for incoming production:
| Sample type | Purpose | Acceptance action |
|---|---|---|
| Molded color reference | Master color | Reject batch if delta E > agreed limit |
| First-article function sample | Functional verification | Hold production until approved |
| 1% production check | Ongoing quality sampling | Escalate if >2 fails in 30 samples |
Module 6 — Packaging, labeling and function-specific QC checks: finalize retail presentation and testable QC points
Packaging and labeling are part of the product experience and may carry legal or compliance text depending on your market. Buyer actions: supply artwork and packaging specifications (materials, printing method, die-lines) and define what must appear on packaging (brand, barcode, instructions, warnings) for your markets 2 3. Supplier inputs to request: dieline proof, packaging material certificates (e.g., fiber content for cartons), and a packaging validation sample for shelf-fit and barcode scannability.
Evidence to accept: printer proofs, a production-ready packaging sample, and a final label content approval signed by the buyer. Tradeoffs: custom printed packaging and premium finishing raise unit costs and lead times; plain cartons or labels reduce upfront cost but can reduce retail impact. Next steps: finalize packaging art at least one tooling cycle before P2 sampling so packaging and product validation can proceed together.
Function-specific QC must be defined as measurable checkpoints in production. Buyer actions: define critical-to-quality (CTQ) points for your SKU (e.g., wall thickness, opening diameter, squeaker retention force as a pass/fail metric) and request a QC plan showing inspection frequency and acceptance sampling. Supplier inputs to request: in-process inspection forms, measurement equipment used and calibration records, and the proposed non-conformance flow (segregation, rework, disposal). Evidence to accept: a QC checklist tied to the approved CAD and packaging, and results from a pre-production run that demonstrate compliance with your CTQs. Next steps: include routine lot inspection and sample retention clauses in your purchase agreement so you have records for traceability.
Final buyer checklist — immediate next steps
- Finalize the product role brief and CAD with tooling split lines.
- Require material declarations (trade name + compounder) and retain material datasheets.
- Decide tooling ownership and sign a tooling annex with sample milestones.
- Define color tolerances and require a molded color master sample.
- Approve packaging dielines and define CTQs with measurable acceptance criteria.
Notes on compliance and records
- Distinguish between a supplier’s quality-management system and SKU conformity; a system certificate does not replace SKU-specific evidence like material declarations and FAI results 1.
- Confirm GTINs and product data requirements for your retail channels early in the process; include packaging weight/dimensions and label content in the spec package 2.
- Buyers/importers must confirm specific target-market labeling, testing and import requirements for final product readiness 3.
Module 7 — Packaging choices and buyer decisions for retail vs. bulk distribution
Packaging often drives tooling, MOQ, and unit cost decisions for private label rubber pet toys. For retail-ready items you will need to specify hang-tab types, cardback dielines, blister shapes or windowed boxed designs that protect the toy, present the brand, and meet retailer shelf-space constraints. For bulk distribution (case-packed pallets destined for fulfilment centres or pro retailers) the priorities shift to carton-strength, inner packaging that prevents deformation, and SKU labelling for warehouse scanning. Provide your pack spec early so the factory can confirm whether the intended package fits within the tool-part layout (e.g., toy orientation in a thermoformed tray or polybag), and whether secondary tooling (cardboard insert dies, clamshell trim) is needed.
Sustainability, regulatory labelling and end-customer convenience also affect packaging engineering. If you plan printed instructions, warnings, or multilingual text, include final artwork and required language set at the RFQ stage so proofing and pre-production samples reflect the actual pack copy. For e‑commerce single-unit shipping, include inner void-fill or resealable film options to protect high-compression rubber toys; for subscription or multi-unit bundles, consider partitioned trays or corrugated dividers that prevent rubbing and deformation during transit. Link package-test expectations such as drop, compression and vibration tests to your acceptance criteria 5. The factory will usually quote packaging options separately from unit tooling and provide guidance on cost-effective pack formats compatible with production rates.
Module 8 — Colour, surface finish and buyer decisions for brand fidelity
Colour communication is a frequent source of rework. For private label rubber pet toys you need to decide whether you’ll accept standard factory colour cards, Pantone-matched masterbatches, or printed surface decoration (pad/ink printing or in-mould labelling). Specify whether colour must match a brand swatch under a defined light source and tolerance (e.g., Delta E target) or whether spot variations are acceptable between production lots. If your brand relies on tightly controlled shades, request a colour-control plan that includes masterbatch artwork, approved lab dip(s), and batch-level QC checks; confirm whether the factory will retain masterbatch records and produce re-colour runs from saved recipes.
Surface finish and texture affect both appeal and function. Decide if you want matte, satin, glossy, or textured zones (e.g., grip ridges, simulated fur pattern) and identify which finishes require secondary operations such as pad printing or post-mould painting. For bi-colour or multi-material toys, clarify overmoulding or assembly sequences, and whether colour bleed or flash acceptance is allowable at mould parting lines. Include photographic or physical references with your RFQ so vendors can propose the correct moulding and finishing approach and estimate any additional inspection points to control surface defects.
Module 9 — Samples, approval gates and buyer decisions for sign-off
Your approval workflow determines how many sample rounds are practical. For private label rubber pet toys set gates that reflect risk: a pre-production (PP) sample to check tool accuracy and assembly, a colour/match sample (lab dip or painted proof) to confirm brand fidelity, and a first article inspection (FAI) batch before mass production. Decide whether you will accept digital confirmations followed by 2D sample photos, require physical samples shipped for tactile checks, or mandate in-market pilot testing. Remember shipping time and customs for physical samples can extend lead time; include sample-shipping expectations in your project timeline.
Define acceptance criteria for each gate: critical dimensions within a specified tolerance, freedom from mould lines in critical areas, material appearance and durometer match, and pack fit. Where applicable, require photographic recording and a signed sample approval form that the factory retains in the lot file. If you plan to test toys with third-party labs, schedule that testing after the FAI but before bulk release so any remedial tooling or material changes can be implemented without scrapping significant volume. Align sample count and approval timeline with commercial milestones so tool corrections or colour remakes do not jeopardize launch windows 4.
Module 10 — QC checkpoints, inspection frequency and buyer-specified acceptance
Create a layered inspection approach for private label rubber pet toys that separates cosmetic, dimensional and functional checks. Cosmetic inspections look for surface blemishes, flash, discolouration and consistent texture; dimensional checks verify critical mating features (e.g., holes, threads, snap-fit geometry) and overall tolerances; functional checks examine intended mechanical behaviours such as compression rebound or parts engagement where applicable. Decide which attributes are critical-to-function (CTF) and require 100% inspection or statistical sampling, and which are cosmetic and acceptable under a defined defect classification. Provide the factory with your defect-table thresholds and whether you will follow AQL-style sampling or a stricter zero-defect policy for certain features.
Inspection frequency should reflect risk and production stage. For initial runs, propose line-side monitoring, in-process first-piece checks, and a final random sample inspection before shipment. For established SKUs with stable tooling, switch to periodic audits and lot-sampling—unless a customer complaint or trend flags regression. Specify whether you will use third-party inspection agents, require factory-run internal inspection records, or demand full traceability for batches (material lot number, masterbatch batch, tool cavity ID). Include acceptance actions: rework thresholds, rejection protocols, and corrective action timelines. Tying QC checkpoints to shipment release prevents unexpected returns and aligns with trade handover terms you define with the vendor and logistics partner 6.
| QC area | Typical check | Buyer decision needed |
|---|---|---|
| Critical dimensions | Calipers/go-no-go gauges | Tolerance bands and sampling plan |
| Surface finish | Visual under defined lighting | Defect classes and acceptable counts |
| Colour match | Lab-dip comparison or spectrophotometer | Delta E or visual pass/fail rule |
| Package fit | Trial pack of sample units | Pack orientation and cushion spec |
| Traceability | Batch and tool-cavity records | Retention period and audit access |
Module 11 — Shipping, labelling and buyer decisions for logistics handover
Decide the commercial terms early: who pays and organises export packaging, which party is responsible for inland freight and customs clearance, and the agreed handover point (e.g., factory gate, port of origin) so each side understands responsibility for risk and cost. These logistics choices affect how the factory packs carton quantities, palletizes SKUs, and prepares export documentation. If you require specific pallet patterns, mixed-SKU pallets, or retailer-ready bundling, include those constraints in the commercial contract and packing list so the factory can prepare consolidated or segregated shipments as requested.
Label and documentation controls are part of shipment handover. Specify the exact carton labels, pallet stickers, and SKU barcodes required by your warehousing partner or retail customer. Provide final shipping marks, certificate copies and any special packing declaration forms at the PO stage to avoid last-minute delays. Also decide whether you need factory-level photos of packed cartons, a pre-shipment inspection report, or scan-confirmation of pallet weight and carton counts before release. For cross-border moves, confirm whether the factory will handle export customs clearance or simply provide the required export paperwork for your freight forwarder, and align responsibilities against agreed trade terms 6.
Frequently asked questions
Q: How many pre-production samples should I expect for a private label rubber pet toy? A: Define sample rounds by approval gates—typically one tooling-fit sample (PPAP/FAI), one colour/finish sample, and a small pilot lot for pack validation. Specify whether physical samples are mandatory or photo approvals are acceptable to shorten cycles.
Q: Should I control the masterbatch recipe for colour-critical items? A: If brand colour fidelity is critical, require documented masterbatch records and retention of a sample masterbatch on file, and include a recolour plan in your contract. Confirm this requirement with the factory during RFQ and include it in the tooling and production SOW 4.
Q: What QC sampling method is best for cosmetic versus functional defects? A: Use different strategies: AQL (statistical) sampling may suit cosmetic issues, while CTF features and safety-related functional checks often need 100% verification or tighter sampling rules. Specify defect classification and sampling method up front.
Q: How do I reduce the chance of colour mismatch between batches? A: Ask for a colour-control plan that includes masterbatch storage, batch lab-dip approvals, spectrophotometer readings (if required), and batch-level colour checks. Build a rework/remake threshold into your acceptance criteria and request recorded colour data per lot 4.
Q: Who handles packaging durability testing for transit? A: Decide whether the supplier will perform or arrange drop/vibration/compression tests, or whether you will contract an external lab. Include expected test standards and acceptance criteria in the procurement plan and reference any required reports for shipment release 5.
Q: How do I ensure the factory meets my shipping documentation needs? A: Provide final label artwork, packing lists, and any required certificates at PO issuance. Specify whether the factory produces original customs documents or electronic copies only, and confirm the export handover point and responsibilities per your trade terms 6.
Conclusion
Selecting the right options for tooling, material control, colour, packaging and QC will determine whether your private label rubber pet toys launch smoothly and scale predictably. Make decisions early about sample gates, acceptable tolerances, and packaging formats; put those decisions into the RFQ, PO and approval checklists; and align inspection and shipment handover responsibilities with your commercial terms. Clear, documented buyer choices reduce ambiguity and help the factory convert your branding requirements into repeatable production outcomes.
Project-specific regulatory, performance and testing requirements must be confirmed by the buyer/importer for each order.
Final CTA — Start a controlled pet-toy sourcing conversation with PawViso. Share the product concept, target market, customization route, package direction and estimated order structure for a focused B2B discussion. Email: info@PawViso.com WhatsApp: +86 186 8106 4480 — https://wa.me/8618681064480
Related PawViso resources
- Continue with How to Create a Custom Pet Toy Sampling Plan. Use this pet-toy guide to structure approvals, samples and evidence.
- Browse the PawViso product catalogue to identify product formats for a sourcing brief.
- Follow the PawViso sourcing process and review the B2B buyer FAQ before sharing project requirements.
External reference
For independent product identification and barcode context, review GS1 guidance on Global Trade Item Numbers (GTINs). Confirm the requirements that apply to the selected product, target market and order.