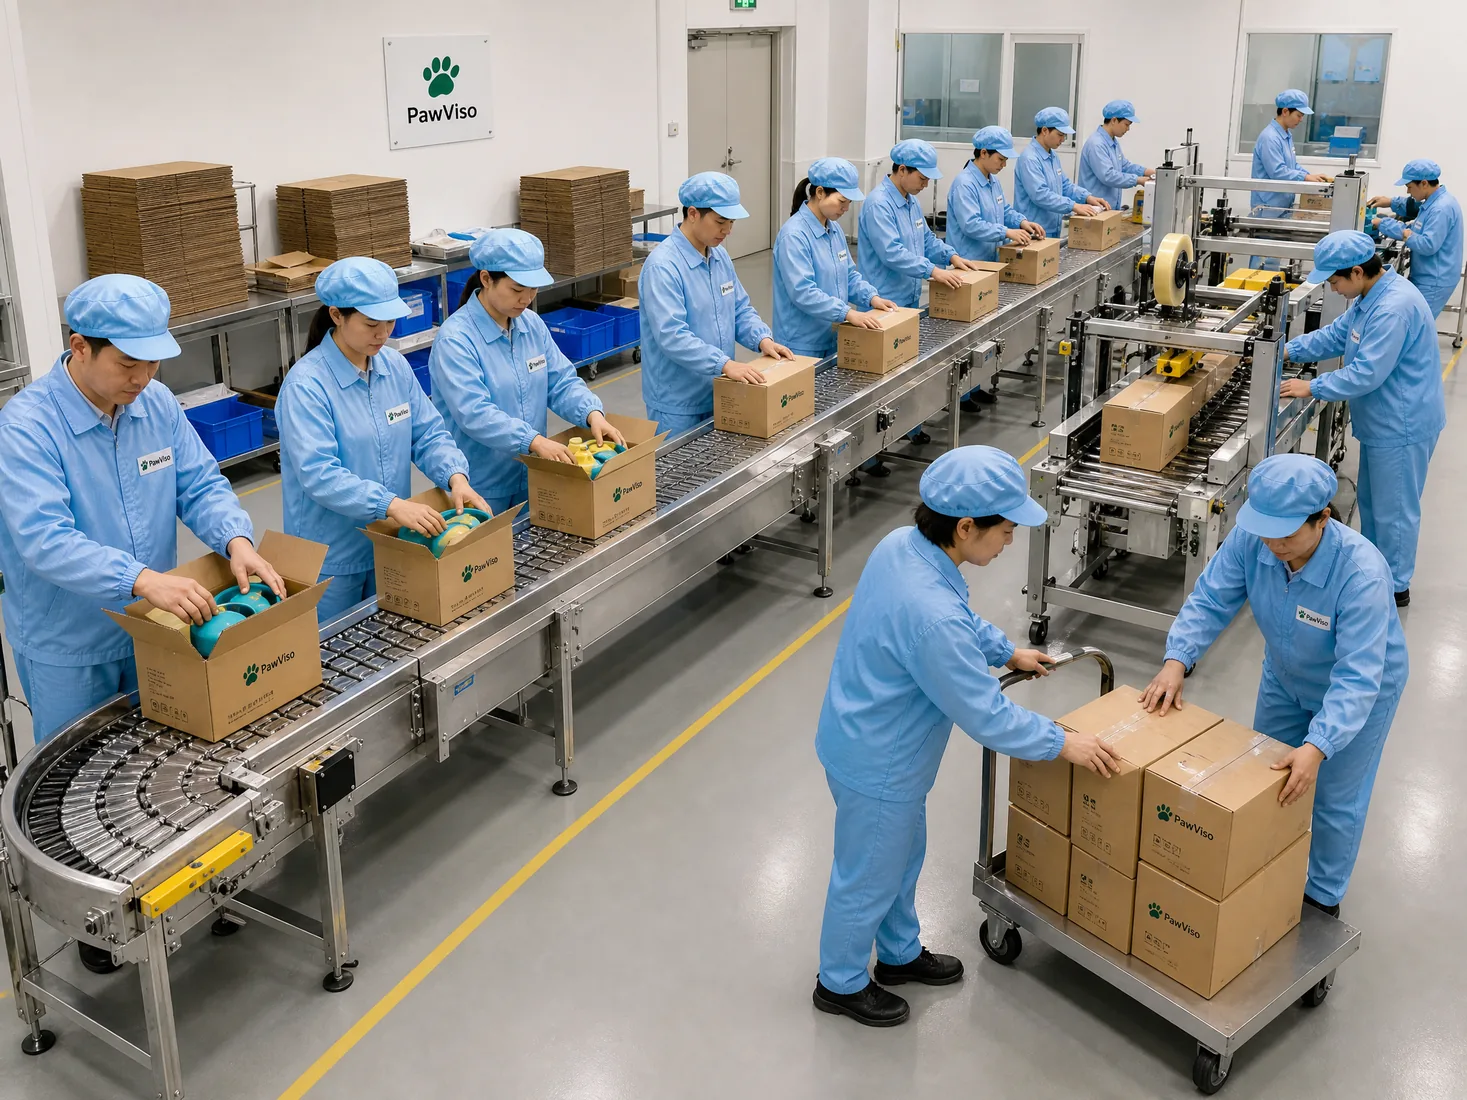
The buyer’s first decision is whether the export carton is being designed for the real distribution route, rather than merely to hold the retail packs. A case that looks efficient on a factory floor can fail at a port handover, warehouse receipt, mixed-pallet transfer, retail replenishment, or parcel dispatch. From a Chinese pet-product factory and procurement partner’s perspective, a shipment-ready carton is a controlled system: the sellable SKU, internal arrangement, outer case, labels, pallet pattern, and records must describe the same physical goods.
Module 1 — Choose the distribution route before specifying the carton
Choose the route first: factory-to-importer warehouse, factory-to-retailer distribution centre, palletized store delivery, or individual parcel fulfillment. Write it as a sequence of handovers, including whether cartons will be floor-loaded, unitized on pallets, transferred through a consolidator, opened at a distribution centre, or shipped onward to consumers. A carton designed for a full, stable pallet of identical cases does not face the same handling exposures as an individually handled parcel or a case placed in a mixed retail pallet. The route determines the protection target, label needs, allowable case configuration, and test discussion.
Ask logistics and receiving teams what happens after port arrival. Record retailer label or pallet rules, and whether e-commerce uses an overbox or the factory case. Put unanswered transfers in the route brief before quotation.
| Route role | Buyer decision to record | Carton-planning consequence | Evidence to keep |
|---|---|---|---|
| Direct import to buyer warehouse | Whether cases stay closed until put-away | Case labels and count must support warehouse receiving | Route map and receiving instruction |
| Retail distribution centre | Whether cases are mixed, split, or store-picked | Case strength, orientation and retailer label format may change | Retailer routing guide confirmed by buyer |
| Palletized wholesale delivery | Whether like cases remain unitized to one consignee | Pallet pattern, containment and load stability become part of the pack-out | Approved pallet diagram |
| Parcel or e-commerce fulfillment | Whether a retail unit or factory case enters parcel handling | Product protection must address individual-package handling | Channel pack specification |
Module 2 — Define the packaging hierarchy and ownership at every level
Define every physical level from product to shipment unit, and name who controls each one. The hierarchy usually includes the product, any immediate bag or wrap, retail pack, inner pack, export carton, pallet, and the shipment or container load. Not every SKU uses every level. A leash on a card may go directly into an export case, whereas a fragile feeder may require a fitted insert, retail box, protective inner arrangement, master carton, and pallet. The buyer should not use “carton,” “box,” and “master” interchangeably because each word can mean a different level to a factory, freight forwarder, or retailer.
Create one hierarchy sheet for each SKU or defined family, with purpose, quantity, identifier if required, and owner at each level. The factory can propose assembly; the buyer or importer should own commercial configuration, market information, receiving requirements, and approval authority. For pet-food or treat contact packaging, confirm the contact-material requirement separately; FDA includes food packaging and components among food-contact substances.1
| Packaging level | Primary purpose | Buyer must decide | Factory or procurement partner should document |
|---|---|---|---|
| Product and immediate protection | Keep the defined product and accessories together | Included components and any contact-material requirement | Component list and packing sequence |
| Retail pack | Present the consumer unit | Sellable quantity, artwork revision and assembly appearance | Retail-pack work instruction |
| Inner pack | Group or separate retail packs where needed | Whether it is a receiving or replenishment level | Inner quantity, orientation and label requirement |
| Export carton | Protect and transport a fixed case quantity | Case count, marks, dimensions target and route | Case drawing, packing diagram and closure method |
| Pallet or logistics unit | Enable handling and traceability | Pattern, height limit, containment and receiver labels | Pallet plan and loading photograph requirement |
Module 3 — Set case count from handling, replenishment, and damage risk
Set the case count by the receiving unit and product geometry, not by a round number or an untested maximum fill. Begin with the quantity that a receiver wants to order, receive, or replenish, then test whether that quantity allows a workable carton footprint, safe product arrangement, manageable weight, and enough protection. The correct count for a low-profile cat teaser differs from the correct count for filled travel bottles, soft beds, ceramic feeding accessories, or bulky scratch products. A single assortment may justify more than one case count when variations have materially different dimensions or protection needs.
Ask four direct questions before fixing the count: Can a person or handling system move the case through the intended route? Will a full case fit the warehouse and pallet pattern? Does the arrangement leave voids or force product compression? Does the count match how the customer receives or sells stock? A dense case can reduce empty volume but create a greater likelihood of crush, scuffing, or incorrect picking. Conversely, a low count may simplify handling but multiply labels, cases, and receiving touches. The buyer should assess those trade-offs against the actual customer workflow rather than demanding the highest possible pieces per carton.
| Case-count question | Acceptable buyer record | Typical failure if omitted | Release action |
|---|---|---|---|
| What exactly is inside? | SKU, variant, components and units per case | Mixed colors, missing accessories, wrong bundle quantity | Reconcile against the purchase order |
| How are units arranged? | Numbered packing diagram and orientation | Movement, abrasion, bent cards, unbalanced case | Review physical trial pack |
| Is the case homogeneous? | Explicit homogeneous or mixed-case designation | Warehouse scans one SKU but receives another | Define separate label and receiving treatment |
| What is the handling unit? | Receiver’s case and pallet instruction | Case count conflicts with store or warehouse process | Confirm with the receiving party |
Module 4 — Lock dimensions, weights, and cube with a physical pack-out
Approve outer dimensions and weights only after a physically packed configuration exists. Retail-pack dimensions, a supplier’s catalogue case, or a computer layout can begin the discussion, but none proves the final export case. Measure an assembled case containing the agreed products, inserts, dividers, labels, and closure. Record external length, width, height, tare weight, gross weight, net product weight if relevant to the buyer’s process, and case count. Link these figures to the packing diagram and revision, because a new leaflet, insert, bottle cap, or divider can change the outcome.
Dimensions are operational data. The buyer uses them for container planning, freight estimates, warehouse slotting, label creation, and pallet design. The factory uses them for board cutting, packing instruction, and line setup. If figures are estimated at quotation stage, label them estimated; do not merge them into final shipping data. Once approved, any change in case count, retail-pack size, carton construction, or protective material should trigger a review of the physical measurements and pallet pattern.
| Measurement record | Why the buyer needs it | Source of truth | Change trigger |
|---|---|---|---|
| External case L × W × H | Freight, pallet plan and warehouse fit | Measured, fully closed physical case | Carton or internal-pack revision |
| Units per case | Ordering, labels and stock reconciliation | Approved pack-out sheet | SKU mix or arrangement change |
| Gross case weight | Handling and transport planning | Weighed, packed physical case | Product, accessory or protective-material change |
| Pallet footprint and pattern | Load stability and receiving fit | Buyer-approved pallet diagram | Case dimensions or receiver change |
Module 5 — Select protection by the damage mechanism, not by appearance
Match protection to the failure that the route is likely to create: movement, impact, compression, abrasion, moisture exposure, or loss of components. First identify which product surfaces are vulnerable and when. A clear retail window may scratch when units rub together. A ceramic or glass component may need separation and support. A metal grooming head may abrade a printed card. A multi-piece play set may need a counted inner bag so small parts do not migrate through the case. Protection should restrain, separate, cushion, or contain the product for an identified reason.
Avoid specifying a material solely by a photo reference or a vague instruction such as “add more padding.” State what it must do, where it goes, and how the operator verifies it. For example, “one divider between each row, fitted in the direction shown on the packing diagram” is inspectable. “Better protection” is not. If the buyer has material restrictions, sustainability objectives, recyclability expectations, or destination requirements, record the confirmed requirement separately from the protective function. The European Commission’s packaging framework covers packaging design, composition, and recoverability issues, but the buyer must determine how the applicable requirements affect the actual materials and market placement.2
| Damage mechanism | Protective decision | Verification at pack-out | Evidence to retain |
|---|---|---|---|
| Product-to-product contact | Divider, sleeve, bag, or controlled spacing | Units do not contact at named vulnerable points | Open-case photographs |
| Free movement in case | Fitted insert, partition, or approved void management | Product arrangement remains as diagrammed after closure | Pack-out sample record |
| Compression of retail packs | Case orientation and stack/load plan | Retail packs stay square and closures remain engaged | Trial-pack and load review |
| Component loss | Sealed inner bag or counted compartment | Every listed component is present before final closure | Component count check |
| Moisture or contamination concern | Buyer-approved barrier or handling arrangement | Required layer is present and intact | Material and assembly record |
Module 6 — Put the full carton scope into the quotation and purchase order
Quote the export-carton system as a defined scope, not as a single line labelled “export carton.” The buyer should ask for the pack-out, outer case, printing, internal protection, labels, sealing method, palletization, inspection, and sample stages to be identified separately. This does not require a supplier to disclose a universal cost formula. It does require both parties to know whether a printed carton, divider, desiccant, pallet corner, label application, or loading photo is included, excluded, buyer-supplied, or pending confirmation.
A clean quote protects sourcing decisions when products, retail packaging, and logistics are developed at different times. It also makes comparison between Chinese factories more meaningful. A supplier that appears lower priced may have assumed a plain carton, no inner protection, a different count, or no pallet work. A buyer should compare like-for-like pack-out assumptions before negotiating. If there is a target price, use it as a commercial constraint after the required route, product protection, and handling scope have been stated.
| Quotation scope | Buyer instruction needed | Supplier response needed | Unresolved-risk signal |
|---|---|---|---|
| Case construction and print | Plain or printed, approved artwork/mark revision | Included material and print scope | “Standard export carton” with no description |
| Internal pack-out | Count, orientation, dividers and component bags | Proposed assembly method and exceptions | Quantity stated with no arrangement |
| Case labels and marks | Content, location, language and ownership | Application step and label source | Label data “to be advised” near shipment |
| Pallet and load preparation | Pattern, containment and receiver requirements | Inclusions and loading method | No decision on palletized versus floor-loaded |
| Validation and inspection | Required sample, checks and release authority | Scope of support and records available | “QC included” without an inspection plan |
Mid-article CTA — Turn carton assumptions into a buyer-ready pack-out brief. PawViso can help structure a SKU-to-carton matrix, pack-out drawing checklist, quotation scope, and pre-shipment records list for a China sourcing project. Email info@PawViso.com with the target market, product list, retail-pack status, route, and receiving requirements.
Module 7 — Approve markings, identifiers, and labels as operational data
Approve carton marks and labels from the receiving process backward, then verify that they reconcile with the physical case. At minimum, decide which identifiers and descriptive information the consignee, warehouse, retailer, and carrier require. Case-level information can include buyer SKU, product description, variant, units per case, purchase-order reference, carton sequence, origin statement where applicable, and directional or handling marks. A mark is useful only when the recipient can interpret it and the production team can apply it consistently at the defined location.
Separate trade-item identification from logistic-unit identification. GS1 explains that cartons and outer cases may carry a trade-item barcode, such as an ITF-14, EAN/UPC, or GS1-128 barcode, whereas a logistic label identifies a logistics unit. Where a GS1 Logistic Label is required, its single mandatory element is a unique Serial Shipping Container Code (SSCC).3 The buyer, barcode owner, and receiver must decide whether an export case is a trade item, a logistics unit, or both. A factory should not generate or reuse identifiers without the authorized party’s instruction.
Use handling symbols only when they communicate a needed instruction. ISO 780:2015 specifies graphical symbols conventionally used on distribution packages to convey handling instructions and says they should be used only when necessary; it does not cover dangerous-goods instructions.4 In practice, select a mark because a specific arrangement, orientation, or condition requires it, not because more symbols make a carton appear more professional. Confirm any carrier, customs, retailer, or destination-specific marks with the responsible buyer or importer.
| Marking decision | Buyer controls | Factory verifies before release | Receiving consequence |
|---|---|---|---|
| Case description and count | Exact SKU/variant wording and units per case | Text matches SKU master and physical count | Correct put-away and stock reconciliation |
| Case barcode | Identifier owner, symbol and required level | Scan result and human-readable digits match record | Reliable case receiving where used |
| Logistics label | Whether a logistics unit and SSCC are required | Label placement and unique assignment process | Traceable pallet or shipment unit |
| Handling marks | Route-specific instruction and approved symbols | Marks are present only where approved | Reduced handling ambiguity |
| Origin or market marking | Importer-confirmed wording, location and scope | Latest approved mark is used | Avoids unapproved assumptions at import |
Module 8 — Use a staged sample gate before mass packing
Do not release full packing from a drawing alone; use staged samples that answer distinct buyer decisions. The first useful gate is a structural or trial pack-out sample. It shows whether the named products, retail packs, protection, count, dimensions, and closure can coexist in the proposed case. The second is a printed or marked carton sample when printing, labels, or externally visible information is part of the requirement. The third is a pre-production packed reference that reflects the released configuration. These samples can sometimes be combined, but their purposes should remain explicit.
At each gate, record the decision: revise, approve conditionally, approve for the next stage, or release for production. An approval should state exactly what is approved and what is not. For example, a buyer may approve a 12-count arrangement while holding the final case print pending a barcode check. A supplier then knows not to treat a positive comment on fit as authorization to print the carton. Retain clear photographs of all faces, the open case, internal layers, closure, and any label position.
| Sample gate | Direct buyer question | Minimum review evidence | What must not be inferred |
|---|---|---|---|
| Trial pack-out | Does the proposed arrangement fit and protect the named units? | Open and closed photos, count, orientation, measured case | Final artwork or test pass |
| Printed-case proof | Does the visible carton information match the approved record? | All-panel proof, mark checklist and scan check where relevant | Final production packing consistency |
| Pre-production packed reference | Does the released system appear correctly assembled? | Physical configuration, records, exception log | Every future lot will conform automatically |
| Palletized sample or mock-up | Does the unit-load plan work for the stated route? | Pallet diagram, label location and containment review | Suitability for another carrier or route |
Module 9 — Select transit tests that match the distribution hazards
Choose a test approach only after defining the shipment configuration, route, and decision the result must support. Do not order a named package test because it appears on another buyer’s specification. The International Safe Transit Association differentiates screening tests from simulation tests and offers procedures for distinct distribution situations. Its 3-Series general-simulation procedures are intended to simulate damage-producing motions, forces, conditions, and sequences in transport environments.5 A test method is therefore a defined tool, not a universal certification of a pet product or its carton.
Start by naming the exact test article: retail pack in an overbox, complete export case, or unitized pallet load. Then name the route assumption: parcel, mixed less-than-truckload shipment, direct import to distribution centre, or unitized truckload. Define pre-test conditioning if relevant, the sample quantity, inspected attributes, acceptance criteria, and who reviews results. If the product or packing method changes after test, the buyer should decide whether the tested configuration remains representative. A report supports only the specimen and scope stated in that report.
| Validation choice | Use it when the buyer needs to decide | Define before execution | Limitation to state |
|---|---|---|---|
| Bench or trial-pack review | Whether arrangement and clearance are workable | Product, pack-out, observed checks and pass criteria | It does not simulate full transport |
| Screening integrity test | Whether a design merits early comparison | Exact sample configuration and benchmark | It is not necessarily predictive of route performance |
| Route-related simulation | Whether the stated package system can be evaluated against stated hazards | Distribution route, procedure, configuration and acceptance criteria | It does not cover unstated routes or substitutions |
| Unit-load review | Whether pallet pattern and containment are workable | Case pattern, handling equipment and load condition | It does not validate individual retail packs by itself |
Module 10 — Inspect the packed lot against records, not memory
Inspect finished packing against the approved case specification, purchase order, and released sample before shipment release. The inspection needs both product-level and carton-level coverage. At carton level, check SKU and variant identity, unit count, internal arrangement, protective components, external dimensions where required, closure, labels, carton marks, barcode scan where applicable, and visible condition. At load level, check the agreed pallet pattern, label application, containment, and condition of accessible cartons. The inspection plan should state what is sampled, how cartons are selected across the lot, and who may accept, hold, rework, or release.
A carton inspection is not a generic “packaging passed” statement. It compares each observation with an agreed requirement. If a divider is critical to product separation, define its location and presence as a check. If a retailer requires a label on a specific case face, define the face from the viewer’s perspective and record it. If cartons have sequence numbers, check their continuity or stated allocation rule. Where a supplier uses an acceptance-sampling approach, the buyer must determine the lot identity, sampling policy, defect definitions, and action rules; a sample result does not prove that every unit is defect-free.
| Inspection area | Control question | Record to capture | Example hold condition |
|---|---|---|---|
| Case identity | Does the case contain the ordered SKU and variant? | Case mark, opened-carton check and PO reference | Case text and physical contents disagree |
| Pack-out | Are count, orientation and protection per the released diagram? | Count sheet and open-case photographs | Divider or listed component missing |
| Closure and condition | Is the case closed as specified without visible damage? | Closure method and defect photographs | Open seam, crushed corner, or wet carton |
| Labels and marks | Do printed data and applied labels match approved records? | Panel check and scan result where relevant | Wrong data, unreadable code, or label on wrong face |
| Pallet and load | Does the unit load match the approved plan? | Pallet photo, pattern and containment record | Unstable overhang or unapproved mixed configuration |
Module 11 — Release loading only when the shipment matches the approved configuration
Treat loading readiness as a separate release decision after the cartons and logistics instructions are complete. Before a container is loaded or a collection is handed to a carrier, reconcile the purchase order, packing list, case count, carton sequence if used, pallet count, shipping marks, and loading plan. Confirm whether the goods are floor-loaded or palletized, which party applies any final labels, and what photographs or seal records the buyer requires. A container can be full while still being wrong for the buyer if cases are mixed without instruction, labels are inaccessible, or the loaded quantity does not match the packing list.
The loading plan should define placement rules that are relevant to the product: orientation, stack pattern, separation of fragile or crush-sensitive cases, treatment of empty spaces, and access to required labels. It should also explain what happens if the planned quantity changes. A last-minute partial shipment can create instability or force an unapproved mixed load. The factory or freight party should escalate the difference for buyer direction rather than improvising a new configuration without a record.
| Loading-release record | Buyer decision supported | Responsible confirmation | Escalate when |
|---|---|---|---|
| Final carton and pallet count | Does the shipment match the commercial order? | Factory and buyer/forwarder reconcile documents | Count differs from packing list or PO |
| Loading configuration | Is the route-specific plan followed? | Loading team records palletized or floor-loaded method | Plan cannot be followed as approved |
| Condition and label visibility | Are accessible cartons and logistics labels usable? | Loading photographs capture key faces and load condition | Damage, obscured labels, or unapproved orientation appears |
| Shipment traceability | Can records link goods to the released configuration? | Lot, carton, label and loading records are retained | Revision or sequence cannot be reconciled |
Frequently asked questions
Can one export carton work for retail, wholesale, and e-commerce?
Possibly, but only after the buyer defines every route and confirms the same system serves each one. Retail, wholesale, and parcel handling can impose different hazards and receiving needs.
Should the factory select the carton dimensions and case count?
A Chinese factory can propose the configuration, but the buyer should approve it after reviewing the physical pack-out, measurements, route assumptions, and quotation scope. Conflicts should be escalated, not changed silently.
What should be on a pet-product export carton?
Include only information needed for the agreed import, receiving, and transport process. The buyer or importer must confirm required wording, identifiers, language, and placement for the actual market and customer.
Is a passing transit test enough to release the shipment?
No. It addresses only its stated specimen, procedure, route assumptions, and criteria. Shipment release also needs confirmation of finished goods, pack-out, labels, quantity, and loading instructions.
Conclusion
Plan pet product export cartons as a controlled distribution system, not as the last packaging line on a purchase order. A buyer who first identifies the route can then set a defensible hierarchy, case count, dimensions, protection, marks, sampling gates, validation scope, inspection checks, and loading records. For a Chinese pet-product factory or procurement partner, the most valuable input is a decision-ready brief that names the SKU, packaging revision, receiver, route, and release authority. That brief allows the factory to propose workable alternatives without silently changing the buyer’s commercial or logistics intent.
Final CTA — Plan the next shipment with a documented carton brief. For structured support on pet product export cartons, pack-out records, proof-sample gates, and shipment-readiness questions, contact PawViso at Email: info@PawViso.com or WhatsApp: +86 186 8106 4480.
This article is general B2B sourcing information. Project requirements, including product, market, packaging, route, testing, marking, inspection, and import requirements, need buyer/importer confirmation for the actual SKU and shipment.
Related PawViso resources
- Continue with How to Prepare Pet Product Packaging Artwork. Use this guide to organize artwork, barcode and pack-out inputs.
- Browse the PawViso product catalogue to identify product formats for a sourcing brief.
- Follow the PawViso sourcing process and review the B2B buyer FAQ before sharing project requirements.
External reference
For independent shipping-term and handover context, review International Chamber of Commerce Incoterms® 2020 overview. Confirm the requirements that apply to the selected product, target market and order.
References
- 1Food Packaging & Other Substances that Come in Contact with Food - Information for Consumers
- 2European Commission: Packaging Waste
- 3GS1 Logistic Label Guideline
- 4ISO 780:2015 Packaging — Distribution packaging — Graphical symbols for handling and storage of packages
- 5International Safe Transit Association Test Procedures