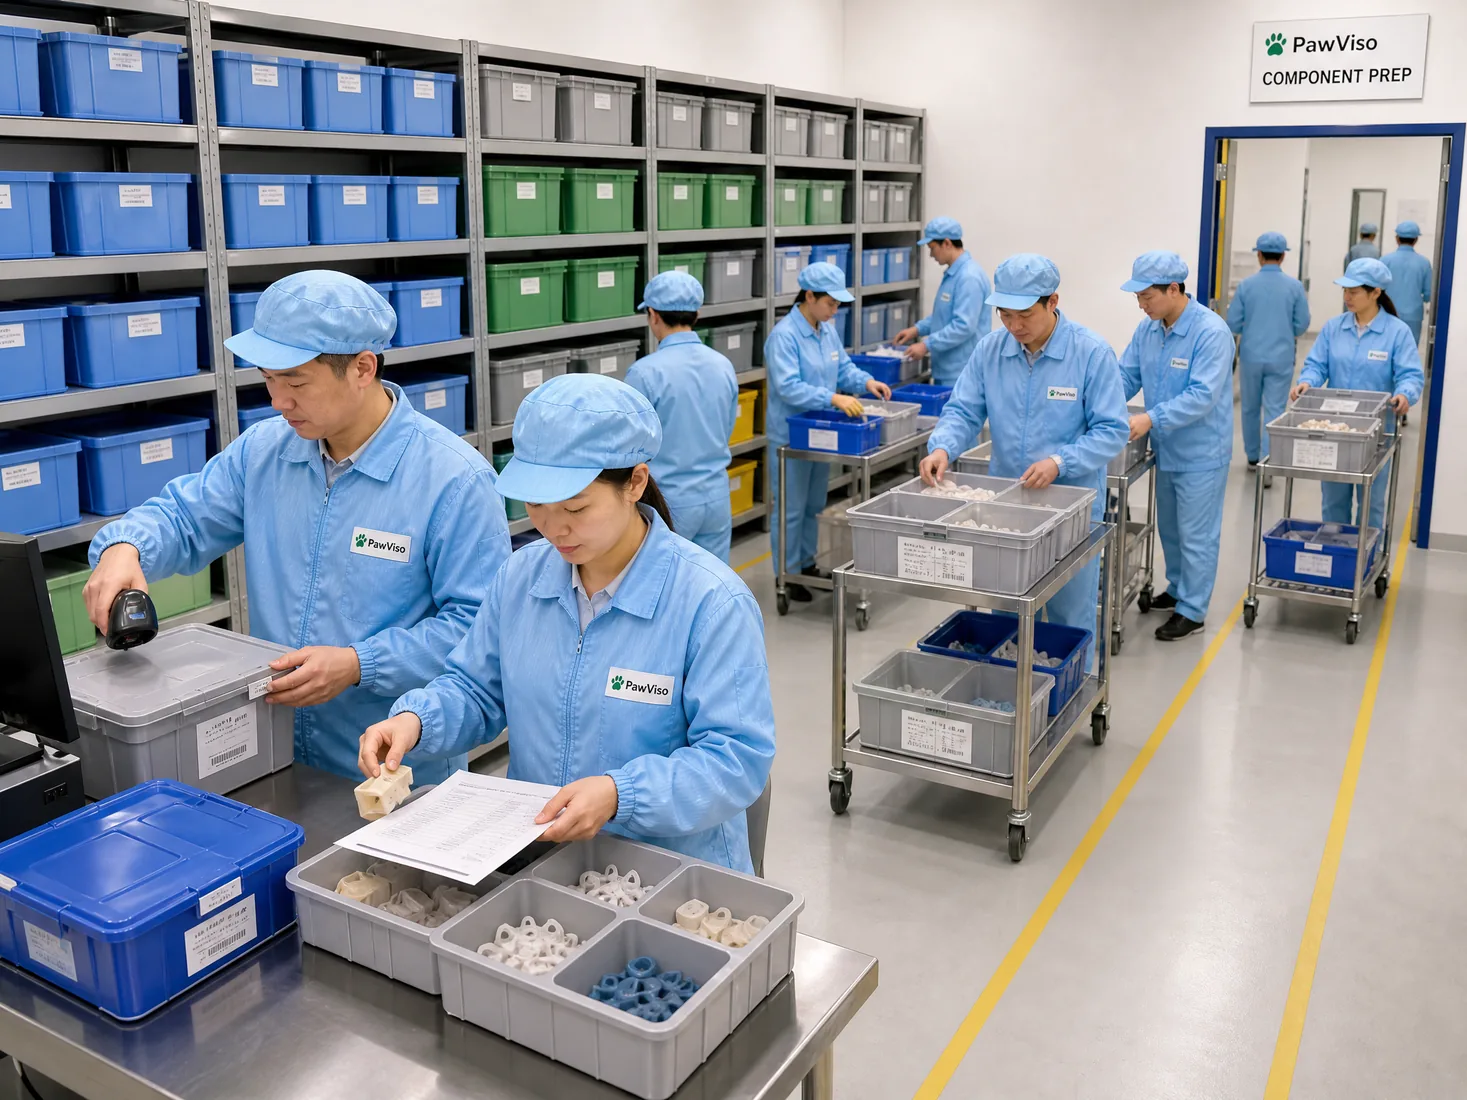
Component traceability for pet toys means keeping a clear, auditable link between every SKU you buy and every physical part, supplier, artwork, and batch that contributed to the finished unit. For procurement teams, traceability is a business control: it reduces rework, speeds investigations when problems arise, supports supplier accountability, and preserves product continuity across design changes. This guide focuses on the practical records, codes, and handoffs you should require and how to manage tradeoffs between granularity, supplier burden and operational cost.
Traceability is not one single document; it’s a system of connected records that flow from design to shipment. You will decide the level of detail you need for each product family and market, whether to track down to lot/batch level for raw materials, how to link samples and inspection evidence to specific production runs, and how to record version changes to artwork, packaging and component specs. This guide is organized into six modules you can apply sequentially or pick as needed for different SKUs.
Module 1 — Define the traceability scope per buyer decision: SKU granularity, BOM depth and supplier codes
Start by deciding how granular traceability must be for each SKU. At minimum, determine whether you will track the finished SKU only, or every sub-component (outer packaging, insert, squeaker, cloth panel, dye lot). Practical buyers typically group SKUs with identical designs and constituent parts into families and set different traceability levels per family. Consider factors such as complexity of the toy, history of quality incidents, and destination-market documentation requirements you must confirm with the importer or local compliance team 3.
Ask suppliers to provide a master bill of materials (BOM) that lists each component, its supplier code, material description, control attributes (e.g., colorant batch, fabric lot) and expected supplier contact. Specify which attributes are mandatory for traceability (e.g., supplier code, component part number, date code) and which are optional (e.g., raw-material supplier lot). Request evidence: BOM signed by supplier, component samples linked to BOM entries, and supplier contact details for each component. Tradeoffs: deeper BOM depth increases administrative work and supplier pushback but improves root-cause precision. If you require batch/lot-level traceability for certain components, clarify this explicitly in the purchase agreement and acceptance criteria.
Helpful practical next steps:
- Create a template BOM that requires supplier codes and part-level descriptions.
- Define “traceability tiers” (e.g., Tier A: full component + batch trace, Tier B: component-level only) and assign each SKU family to a tier.
- Require suppliers to map their internal part codes to your SKU and BOM entries at PO time.
Example table: component mapping template
| Buyer SKU | Component name | Supplier code | Supplier name | Traceability tier |
|---|---|---|---|---|
| PT-001 | Squeaker assembly | SUP-1234 | XYZ Squeakers Co. | Tier A |
| PT-001 | Outer fabric panel | FAB-77 | ABC Textiles Ltd. | Tier B |
Example table: BOM required fields for supplier submission
| Field | Mandatory? | Format/Notes |
|---|---|---|
| Component part number | Yes | Alphanumeric, supplier and buyer mapping |
| Supplier contact | Yes | Name, email, phone |
| Material description | Yes | Include color and composition |
| Batch/lot number | Conditional | Required for Tier A components |
Module 2 — Assign stable identifier systems per buyer decision: SKU, internal part codes and supplier codes
Choose and document the identifier system that will be the “single source of truth” for each traceability object: finished SKU, internal part code, supplier part code, and pack/box identifiers. Define which identifier appears on what document (PO, packing list, inspection report). The buyer must decide whether to adopt supplier part numbers as definitive or to issue internal part numbers that suppliers must reference. Using buyer-issued internal part numbers reduces ambiguity but creates an extra mapping step for suppliers.
Require each supplier to include both their internal code and your internal code on all submissions (samples, labels, inspection reports). Supplier inputs should include a standardized product data sheet that lists all identifiers and the relationship between them. Evidence to collect: an identifier mapping table signed or acknowledged by the supplier, sample labels showing both codes, and inspection reports that reference the agreed identifiers. Tradeoffs: enforcing buyer-only codes improves internal consistency but demands process setup; allowing supplier codes reduces supplier friction but increases reconciliation work in your systems.
Practical next steps:
- Publish an identifier policy showing which codes go on which documents.
- Add a mandatory “identifier verification” step to first production inspection: inspector confirms codes on product match the mapping table.
- Keep a version-controlled mapping file accessible to relevant teams (sourcing, quality, logistics).
Example identifier mapping table
| Buyer SKU | Buyer part code | Supplier part code | Doc where code appears |
|---|---|---|---|
| PT-002 | BPC-200 | SUP-556 | PO, Packing list, Inspection report |
| PT-002 | BPC-201 | SUP-559 | Artwork, Label mockup |
Module 3 — Link samples, approvals and artwork versions per buyer decision: sample IDs, approval dates and version control
Decide how you will link pre-production and retention samples to production lots. Buyers should require suppliers to issue sample IDs that tie directly to the BOM and artwork version used to make the sample. For color-sensitive pet toys and packaging, link dye lot references and artwork file version numbers to the sample ID. Supplier inputs include photographed samples with visible sample ID and dated approval sign-offs, plus the artwork file name/version used for production.
Define a version-control rule: each change to artwork, packaging dielines, or component spec must create a new version number and be captured in a change log that references impacted SKUs and supplier part codes. Evidence: approved sample photos (with date and sample ID), recorded approval email or signed approval form, and the artwork file saved under the versioned filename. Tradeoffs: tight version control reduces manufacturer errors but extends lead time for changes. If frequent iterations are expected, use clearly defined “emergency change” procedures with temporary approvals and conditions.
Practical next steps:
- Require suppliers to attach a sample ID label and to photo-document samples from multiple angles.
- Insist on approvals that include explicit confirmation of the exact artwork filename/version and dye lot numbers.
- Maintain a change log that links each new version to the effective production date.
Sample-to-version linking table
| Sample ID | SKU | Artwork version | Dye lot | Approval date |
|---|---|---|---|---|
| SAMP-1001 | PT-003 | ART-v1.2 | DYE-45 | 2025-05-10 |
| SAMP-1002 | PT-003 | ART-v1.3 | DYE-46 | 2025-06-02 |
Module 4 — Capture production records and inspection evidence per buyer decision: lot/batch numbers, QC records, and nonconformance links
Decide which production records you will require from the supplier for each shipment. At minimum, request a production summary that lists production dates, production line or machine ID (if applicable), and lot/batch numbers for any Tier A components. For higher-assurance needs, require complete production traveler documentation and raw-material delivery receipts that include supplier lot numbers. Supplier inputs should include QC inspection reports, in-line inspection checklists, and final random-sample inspection images showing the identifiers and sample conditions.
Specify the inspection evidence you will accept: stamped reports from a third-party inspector, factory QC checklists with photographic attachments, or digital inspection logs. Each inspection item should reference the SKU, internal part codes, supplier codes and production lot number so the report is immediately traceable to the BOM. Tradeoffs: insisting on full traveler records increases supplier administrative burden and may move lead time; accepting only final inspection reports is lighter but reduces the detail available during investigations.
Practical next steps:
- Add a verification column to the packing list: inspector confirms lot numbers and links inspection report ID.
- Require photographic evidence that clearly shows lot numbers and at least three distinct product identifiers (SKU label, sample ID, packing code).
- Define retention periods and storage method for inspection evidence (digital repository, file naming convention).
| Production record type | Buyer-required fields | Supplier evidence |
|---|---|---|
| Production summary | Production date, quantity, lot/batch numbers, line ID | Signed summary PDF |
| In-line QC | Checkpoint name, time, defects logged, inspector ID | Digital checklist + photos |
| Final inspection | Inspector report ID, sample images, acceptance/rejection | 3rd-party or factory report |
| Inspection evidence linkage | Required identifiers shown |
|---|---|
| Final inspection photos | Buyer SKU, production lot, sample ID |
| Packing checklist | Buyer SKU, buyer part code, box serial/ID |
| Nonconformance report | Affected lot, component supplier code, corrective action |
**Mid-article CTA — If you want a ready-to-use traceability template and a starter BOM mapping spreadsheet tailored for pet toys, request Module Excel pack from PawViso support. Provide your SKU list and traceability tier choices for a custom template.
Module 5 — Manage change records and approvals per buyer decision: change logs, effective dates and supplier acknowledgments
Decide how changes will be authorized and communicated. Every change that affects a component, artwork, packaging or supplier source must be recorded in a change log with clear effective dates and required supplier acknowledgement. Determine whether minor changes (e.g., minor color adjustment within tolerance) require full reapproval or only documented notification. Buyer inputs should include a change request form that asks for reason, impacted SKUs, and a list of attached evidence (new sample ID, updated artwork file, revised BOM). Supplier inputs are explicit written acknowledgments and, where required, updated samples or pre-production run proofs.
Evidence that a change was properly managed includes: the change log entry, the new sample approval (or a statement of waiver), updated BOM and part-code mapping, and an updated inspection checklist reflecting new attributes. Tradeoffs: tight control on changes reduces downstream variability but can slow the supplier’s ability to optimize processes. To balance speed and control, use tiered change requirements—full approval for Tier A changes, notification-and-record for Tier B. Practical next steps include enforcing supplier acknowledgments in your PO terms and automating change notifications via your supplier portal or shared cloud folder.
Suggested change-log fields
| Change ID | Date | Impacted SKU(s) | Change type | Approval status | Effective date |
|---|---|---|---|---|---|
| CHG-2025-01 | 2025-08-12 | PT-004 | Artwork update | Approved | 2025-09-01 |
| CHG-2025-02 | 2025-08-20 | PT-007 | Supplier source change | Pending | TBD |
Module 6 — Link shipment documents and retention evidence per buyer decision: packing lists, bill of lading, retention samples and archive policy
Decide what shipment-level documents must contain traceability identifiers and how long evidence will be retained. The buyer should require packing lists and shipping documents to include SKU, internal part code, quantity by box, and the production lot/batch number where applicable. If you require container or box serialization, define the box-ID format and require suppliers to print box IDs on both inner and outer packaging. Supplier inputs include signed packing lists, photos of palletized loads with visible box IDs, and shipping labels that show your SKU and PO number.
Retention policy decisions: define how long you will keep digital inspection records, production summaries, and sample photos, and whether you will require a physical retention sample to be held at factory or shipped to a designated location. Evidence to collect for shipments: packing list with linked inspection report IDs, bill of lading showing PO and SKU references, and photos of sealed container/tamper-seal if applied. Tradeoffs: requiring physical retention samples at the factory reduces immediate logistics cost but can complicate retrieval; requiring samples shipped to a central location increases cost and time but centralizes evidence for investigations.
Practical next steps:
- Update PO terms to require lot/batch numbers on packing lists for Tier A items.
- Specify box ID format and enforcement checks at final inspection.
- Define retention period and access rules for traceability records in your contract.
Shipment document checklist
| Document | Must show | Where to store |
|---|---|---|
| Packing list | SKU, buyer part code, lot/batch numbers, box IDs | Project folder in document repository |
| Bill of lading / AWB | PO number, SKU summary, container ID | Logistics folder |
| Retention sample record | Sample ID, storage location, supplier acknowledgment | Traceability archive |
Final practical guidance
- Treat traceability requirements as part of your purchase contract and onboarding checklist. Clear expectations up-front reduce disputes and speed problem resolution.
- Use tiered requirements to balance supplier effort and risk: not every toy needs box-level serialization, but critical components and packaging for higher-risk SKUs should.
- Make sure your teams (sourcing, quality, logistics) agree on the authoritative identifiers and where records live. Centralize records and enforce file naming conventions to avoid mis-matches during investigations.
Notes on quality management and product data Distinguish traceability records from your overall quality-management system: traceability links parts and documents to physical production and shipments, while a quality-management system governs processes, audits and corrective actions—both are necessary but separate controls 1. Also confirm how your GTINs or other product identifiers will be used with product data systems, as GTIN and product-data obligations are buyer-managed decisions for specific markets 2. Finally, always confirm destination-market importer and regulatory documentation requirements with the buyer/importer team before finalizing traceability scope 3.
Module 7 — Component batch and lot linkage
Define buyer decisions: decide whether you require batch/lot-level linkage for every critical component or only for components that carry higher risk (e.g., chemical-treated fabrics, stuffing materials, small parts). This choice affects supplier record-keeping, inspection sampling plans, and how you accept or reject goods on arrival. If you choose full batch linkage, instruct suppliers that every delivered component must show a recorded batch or lot code (machine-printed label, supplier lot ID, or internal factory lot number) that ties back to their raw-material purchase and processing records.
For each component that will be batch-tracked, require a minimum set of trace fields in the supplier handoff: supplier lot ID, supplier production date, incoming raw-material certificates (if provided), and internal in-line process IDs (e.g., dye lot, extrusion run). These fields should be captured in the packing list and the inspection report for every shipment to provide immediate traceability on receipt. If you accept intermittent wholesale shipments that combine lots, specify how the supplier will indicate mixed-lot content and whether segregation will be maintained until you authorize blending.
When you implement batch linkage, create rules for sample retention and quarantine hold periods. Decide how long you will require suppliers and forwarders to retain retained samples and associated testing evidence for each lot. Specify whether retained samples should be stored by the supplier, a third-party lab, or at your warehouse, and state conditions for sample release after successful inspection or testing. This reduces ambiguity when quality deviations arise and ensures quick root-cause work with the responsible lot.
Buyer action checklist:
- Decide level of batch/lot tracking per component and document in the spec.
- Require supplier lot IDs on packing lists and inspection reports.
- Set sample retention duration and custody location.
- Define rules for mixed-lot shipments and blending authorization.
Module 8 — Artwork, labeling and packaging versions
Buyer decision: choose whether packaging artwork and labeling are considered controlled documents requiring formal version control and sign-offs before production. If you treat artwork and package design as controlled, require suppliers to maintain a version history with timestamps, approver names, and version codes on die-lines, proofs, and pre-production samples. This prevents incorrect branding, regulatory text omissions, or incorrect warning statements being printed at scale.
Set specific handoff protocols: require pre-production packaging proofs (digital and physical mockups), final approved print-ready files with version codes, and a photo record of the first-article packaging sample. Insist that the supplier includes the packaging version code on the outer carton label and on the internal batch paperwork so inspectors and receivers can quickly confirm the packaging matches the approved version. For multiple-language packs or country-specific packaging, list each variant as a separate controlled version and tie it to SKUs and shipment destinations.
Manage artwork change requests as formal change orders. Buyers should define an approval workflow (who approves, by what method, and with what timeline). Require that suppliers do not proceed with print or packaging production until the buyer issues written approval of the exact file version. Also decide whether you will accept digital sign-offs (email with file and version reference) or require a project-management system sign-off to be recorded. Document retention and the linkage between packaging version and component lot should be explicit so that, if a packaging error is found in market, you can trace impacted lots and SKUs quickly.
Example packaging trace table (recommended fields)
| Field | Purpose |
|---|---|
| SKU | Links packaging to finished product |
| Packaging version code | Controlled version identifier |
| Approved artwork file name | Exact file approved for print |
| Approval date & approver | Proof of authorization |
| Printer/supplier batch ID | Production-side link |
| First-article photo | Visual confirmation of output |
Module 9 — Sample control and sample-to-production linkage
Buyer decision: determine when a sample becomes authoritative. For pet toy sourcing, the “golden sample” or approved pre-production sample should be the physical standard for quality, dimensions, materials, colors and safety-relevant features. Buyers must state whether the golden sample is binding (e.g., production must match it within defined tolerances) and require suppliers to mark and register golden sample IDs against the relevant SKU and BOM.
Require suppliers to attach sample reference codes to their production orders and inspection documents so inspectors can record which golden sample was used for the comparison. For complex builds with many components, demand a sample hierarchy: a finished-product golden sample plus component-level approved samples (e.g., fabric swatch, molded part sample, closure hardware sample). This allows inspectors to match each component to its approved exemplar during incoming or in-line inspections.
Specify the sample sign-off and revision practice. Define who can request a sample revision (buyer, supplier, or technical partner), how new samples get versioned, and how transitional production is handled when a new sample version replaces an old one. If you permit transitional runs, require explicit documentation indicating which production lots correspond to the outgoing vs. incoming sample versions, and a cutoff shipment where old-version stock is either disposed of, relabeled, or accepted with documented buyer permission.
Practical sample handling decisions:
- Will golden samples be stored centrally by buyer or kept at the supplier?
- Are digital 3D/photographic records required in addition to physical samples?
- What tolerance bands are acceptable for color, dimensions and material properties?
Module 10 — Change records and ECO workflow
Buyer decision: adopt a formal Engineering Change Order (ECO) process for any deviation from the approved BOM, components, or packaging. Without a formal change control process, traceability breaks down rapidly. Your ECO process should require a written change request, an impact assessment (cost, lead time, compliance), sample or mock-up approval, and a final sign-off before the supplier implements the change in production.
Define roles and authority: who in your organization can approve minor changes (e.g., vendor-suggested sub-component swap with no dimension or safety impact) versus major changes (material change, supplier change, artwork redesign). Communicate these authority levels to suppliers and require the supplier to halt production of affected SKUs until proof of approval is presented. Make it clear whether verbal approvals are acceptable (generally avoid) and whether electronic approval systems (PMS, ERP) are the formal record.
Ensure every ECO links forward and backward across records: it should reference the original SKU/BOM/version, the supplier’s lot IDs for affected production runs, inspection results, and any test reports prompted by the change. Store ECOs in a searchable repository so that, if a field issue arises, you can quickly generate a list of all SKUs and lots touched by a given change. For transitional production runs that use pre- and post-ECO components, instruct suppliers to segregate lots and mark cartons with ECO status so warehouse staff and inspectors can distinguish them.
Suggested ECO table columns for buyer-supplier handoff
| ECO ID | SKU | Change type | Effective date | Approved by | Affected supplier lot IDs |
Module 11 — Shipment documents, handover and chain of custody
Buyer decision: specify when and which documents must travel with product shipments and what evidence of handover you require at each step. Typical documents include the supplier packing list with SKU/BOM breakdown, supplier inspection report, supplier lot IDs, packaging version code, and the bill of lading or airway bill. For some buyers, requiring the inspection photos and first-article photos to be attached to the shipment paperwork is a practical control to enable rapid checks on receipt.
Decide how you want the chain of custody recorded: do you accept the supplier’s signed packing list as sufficient, or do you require third-party verification (e.g., independent inspector sign-off at the packhouse, carrier sign-off at pickup)? If you require third-party sign-off, specify the accepted inspection provider or the minimum scope of an independent inspection (count, visual conformance, photos, lot verification). Also make explicit when transfer of responsibility occurs (for example, at supplier’s warehouse, at container stuffing, or when carrier accepts the goods) and reference the trade terms you use in purchase orders 6.
Demand photographic evidence at critical handover points: pre-loading photos of packed pallets, container stuffing photos showing carton orientation and seal number, and photographs of the container seal installed. Request that the shipping label on the outer cartons includes trace fields you've mandated: SKU, quantity, packaging version, and supplier lot IDs if batch-level traceability is required. This reduces disputes at destination and improves the speed of root-cause investigations when non-conformities are detected.
Example shipment handover checklist
| Document / Evidence | Required? | Purpose |
|---|---|---|
| Packing list with SKU/BOM | Yes | Receipt verification |
| Supplier inspection report | Yes* | QA handover proof |
| Photos: pallet, container, seal | Yes | Chain-of-custody visual evidence |
| Bill of lading / AWB | Yes | Carrier responsibility transfer |
| Export customs docs | Buyer-dependent | Import clearance support |
(*Buyer may accept third-party inspection report in lieu of supplier report if specified)
Frequently asked questions
Q: What minimum fields should I require on a supplier packing list to support component traceability? A: At a minimum, require SKU, finished-goods quantity, component list/BOM reference, packaging version code, supplier lot/batch IDs (if tracked), and the supplier production date or lot date. Add an inspection reference (report ID) and the shipment ID (container or AWB) so records link across documents.
Q: How do I handle suppliers who combine multiple component lots into a single carton? A: Decide in advance whether mixed-lot packing is permissible. If allowed, require suppliers to document the lot composition for each carton (carton-level manifest) and to retain evidence that lots were kept segregated during production and packing. If you don’t accept mixing, contractually prohibit it and specify rejection rights.
Q: Should golden samples live with the buyer or the supplier? A: This is a buyer decision. Keeping golden samples centrally with the buyer provides the strongest control but adds logistics and time for on-site comparisons. Leaving them at the supplier speeds on-site checks but may reduce independent control. Many buyers mandate duplicate samples: one retained by the buyer and one kept under controlled storage at the supplier or an independent lab.
Q: How do I make sure artwork changes don’t slip into production? A: Require an explicit artwork approval protocol that includes version codes and an instruction that no packaging print runs proceed without the buyer’s written approval for the specific version. Consider requiring the printer to confirm receipt of the approved file and to include the artwork version code on the final print proof and outer cartons 5.
Q: Can inspection photos replace physical retained samples? A: Photos are a useful supplement but not a full substitute for retained physical samples in most traceability programs. Photos are valuable for quick checks and chain-of-custody evidence; specify which components may be accepted with photos alone and which require physical retention for later testing or dispute resolution.
Conclusion
Component-level traceability for pet toys is a buyer-driven system: define what you track, how it is recorded, and what evidence you require at every handoff. Establish batch linkage, controlled artwork versions, formal sample governance, ECO workflows and clear shipment handover rules to make supplier handoffs auditable and effective. Implement these decisions in your purchase orders, supplier contracts and incoming-inspection checklists so that traceability becomes an operable process rather than an aspiration.
Project-specific requirements — batch rules, compliance needs and market claims — must be confirmed by the buyer/importer for every sourcing project.
Final CTA — Start a controlled pet-toy sourcing conversation with PawViso. Share the product concept, target market, customization route, package direction and estimated order structure for a focused B2B discussion. Email: info@PawViso.com WhatsApp: +86 186 8106 4480 — https://wa.me/8618681064480
Evidence checkpoints
A customization or environmental claim needs a defined scope and supporting evidence rather than broad marketing language.4
Related PawViso resources
- Continue with How to Create a Custom Pet Toy Sampling Plan. Use this pet-toy guide to structure approvals, samples and evidence.
- Browse the PawViso product catalogue to identify product formats for a sourcing brief.
- Follow the PawViso sourcing process and review the B2B buyer FAQ before sharing project requirements.
External reference
For independent quality-management system context, review ISO 9001 quality-management systems overview. Confirm the requirements that apply to the selected product, target market and order.